01 Inspection across the build
- Incoming — wire, terminals and connectors checked against the agreed specification, with supplier records kept for critical materials.
- In-process — first-article check at crimping, patrol inspection at key stations, and a line stop when a result drifts out of tolerance.
- Outgoing — electrical test on every assembly, plus visual and packaging checks against the agreed sampling plan.
02 Electrical and mechanical tests
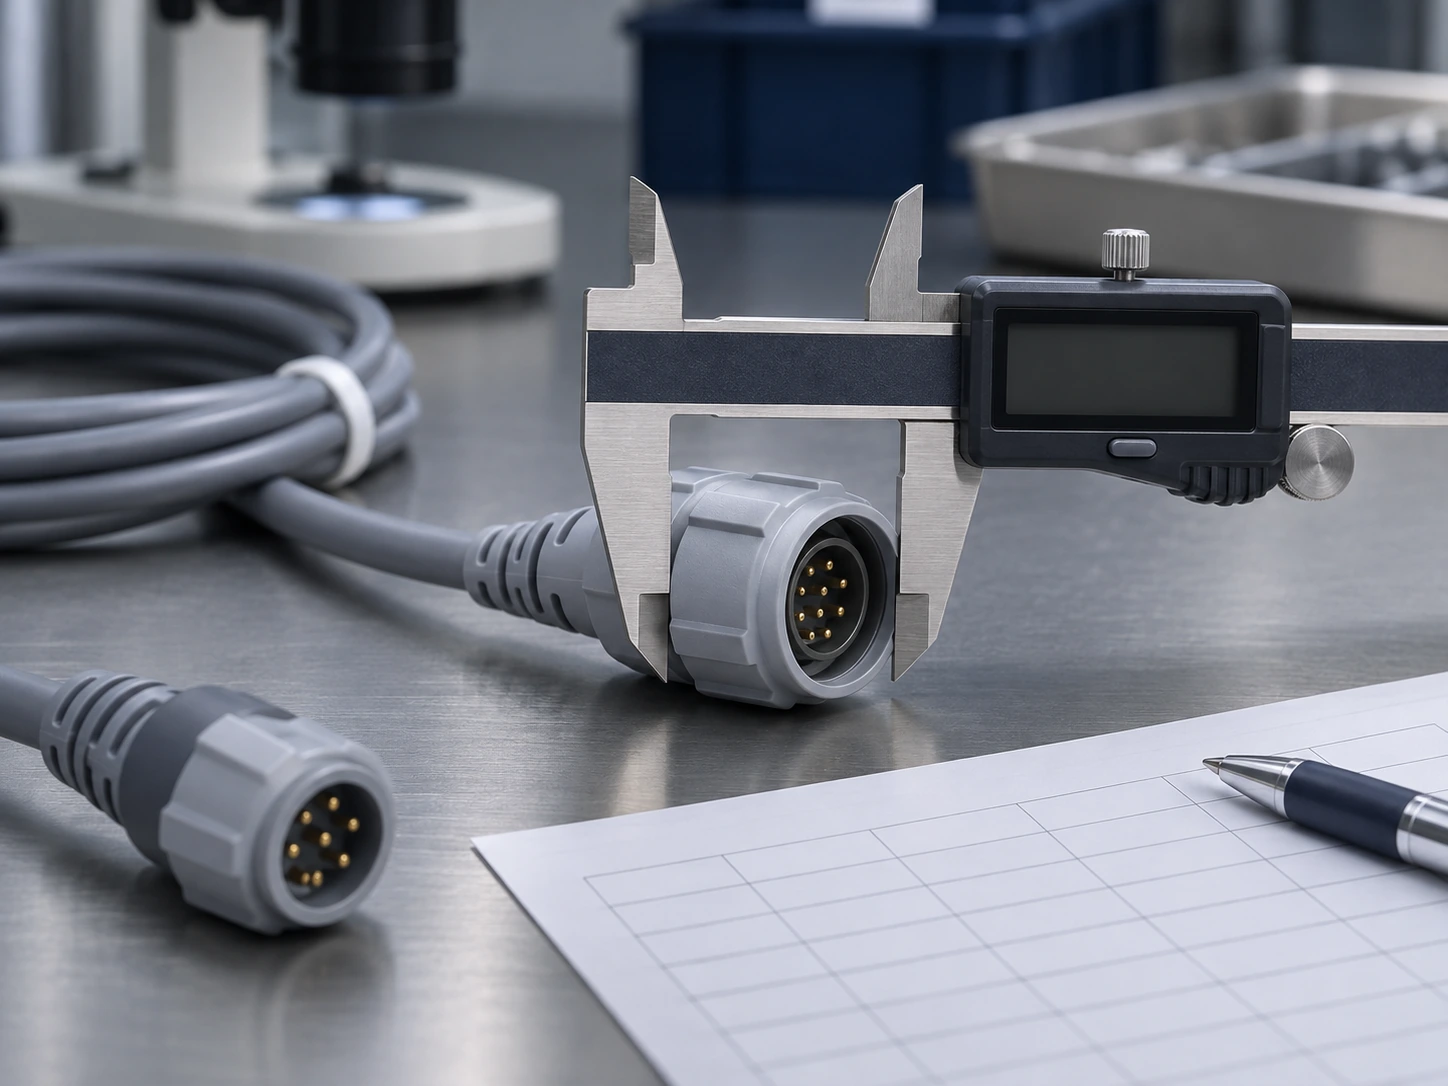
The following are the tests we discuss most often for medical assemblies. Which of them apply, and at what limits, is fixed in the inspection plan for each part number.
- Continuity — every circuit connected correctly, with no opens or shorts.
- Dielectric withstanding — insulation holds the specified voltage without breakdown.
- Insulation resistance — leakage between conductors stays within the agreed limit.
- Pull force — crimp joint and strain relief meet the specified value.
- Contact resistance — consistency at the connector interface.
- Flex life — where the application calls for it, tested to an agreed cycle count.
Test limits and coverage are stated per part number in the inspection plan. We do not publish a company-wide coverage figure.
03 Traceability
Each production lot carries an identifier that links back to material lots, process records and test data, so a question about one shipment can be answered without reconstructing it from memory.
- Lot identifier on the assembly or its packaging.
- Material, process and test data archived against that identifier.
- Retention period agreed per customer and device class.
04 Documentation with the shipment
Inspection reports, test data and certificates of conformity are provided according to what the project agreement specifies. If your quality system requires a particular format, tell us during review so it is built into the process, not added afterwards.